Wednesday, September 10, 2014

Specific Types of Common Corrosion

Carbon Dioxide (Sweet) Corrosion 

Carbon dioxide dissolves in water to form carbonic acid which causes what is known as
sweet corrosion. The product of this form of corrosion is iron carbonate which forms as a film
on the metal surface. At higher temperatures (+80oC) this film has protective qualities leading
to lower than expected corrosion rates at higher temperatures. Sweet corrosion is typically
observed as metal wall thinning and shallow pitting. Under high velocity conditions deep
elongated pits are sometimes observed.

Hydrogen Sulphide (Sour) Corrosion 

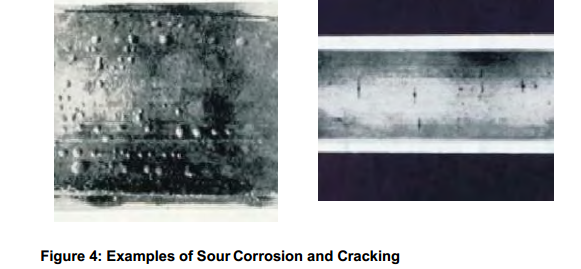
Hydrogen Sulphide dissolves in water to cause what is known as sour corrosion. The product
of this form of corrosion is iron sulphide. The low solubility of iron sulphide in water results in
the formation of a dark or black corrosion product film that is able to protect the steel surface
from general corrosion even in aggressive systems. However due to the conductive nature of
the protective film any local break in the iron sulphide layer can result in very severe pitting.

Hydrogen sulphide may also cause hydrogen damage in susceptible steels. The reaction
which gives rise to the iron sulphide film releases atomic hydrogen which can then diffuse
into the steel where it can lead to the formation of hydrogen blisters or through wall cracking
(Sulphide Stress Corrosion Cracking or Stress Oriented Hydrogen Induced Cracking).

Microbial Corrosion 

Microbial corrosion is caused by the action of bacteria contaminated systems, commonly sulphate reducing bacteria (SRB’s). It is not the bacteria themselves that attack the metal but the local environments that they create and contribute to that leads to corrosion of the structure. Microbial corrosion is typically a problem inside pipes which are left with stagnant water, at dead legs and in the bottom of tanks. For microbial corrosion to occur conditions must be suitable to support bacterial life. These requirements include: 
  • Presence of bacterial life in the system. 
  •  Source of Sulphate. 
  • Source of Carbon. 
  • Source of water. 
  • Anaerobic conditions. 
  • Close to Neutral pH. 
  • Suitable temperature and pressure for bacterial life to be sustained. 

Atmospheric Corrosion 

Moisture, oxygen and aggressive species such as sulphate, nitrates and chlorides present in 
the atmosphere can lead to atmospheric corrosion occurring on exposed structures. 
Atmospheric corrosion proceeds under the same mechanism as wet corrosion however as a 
bulk liquid phase is only present during rainfall the corrosion reactions proceed in a thin film 
of condensed or absorbed moisture on the metal surface. 

The major factors that affect the rate of atmospheric corrosion at a given location are the 
moisture levels and the concentrations of aggressive species in the environment. Marine 
environments for example with high levels of chlorides present would exhibit significantly 
greater corrosion rates than inland environments with low levels of chloride. Similarly 
exposed metal structures in industrial locations with high levels of pollution and therefore 
higher levels of sulphates and nitrates than rural locations would record higher atmospheric 
corrosion rates than would be observed in rural locations. 


Source:http://www.hse.gov.uk/offshore/ageing/ageing-plant-summary-guide.pdf

Monday, September 8, 2014

Common forms of localised offshore corrosion

Pitting corrosion 

Pitting is an extremely localised form of attack where the wall loss is confined to a very small
area of the surface. The conditions within the pit can quickly become increasingly aggressive
causing corrosion pits to rapidly advance through the wall thickness whilst the vast majority
of the pipe or vessel wall remains unaffected. This can lead to very rapid failures as the pit
quickly penetrates the wall. This form of attack is one of the main forms of corrosion
observed in corrosion resistant alloys, however it is also found with corrosion of carbon
steels.

Crevice corrosion 

Crevice corrosion is similar to pitting corrosion, in that it is likely to be observed under the
same environmental conditions that have given rise to pitting. In crevice corrosion the area of
localised attack is found within crevices which typically form around and under washers, bolts
and seals. The solution within the trapped pocket can become increasingly aggressive and
significant localised attack can occur around the crevice.

Galvanic corrosion 

Galvanic corrosion occurs at the junction of two dissimilar metals which are in electrical
contact with each other. According to their relative positions within the galvanic series one
metal will be protected from corrosion at the expense of the other. Depending on the relative
surface areas of each metal this form of corrosion can proceed extremely quickly. If the
cathodic metal is much larger than the anodic metal surface then the observed corrosion
rates can be extremely high as a large cathodic area is driving corrosion at a relatively small
anodic point.


Source:http://www.hse.gov.uk/offshore/ageing/ageing-plant-summary-guide.pdf

Wednesday, September 3, 2014

Type of CUI inspections: Pulsed Eddy-Current (PEC)

Assessing condition of pipework and pressure vessels under insulation can be advantageous to plant operators. The Pulse Eddy Current (PEC)  system was developed as a solution to the detection of corrosion under insulation (CUI) and validated by Shell Global Solutions.

Compared with conventional eddy-current testing, pulsed eddy-current inspection requires no direct contact with the object being tested. Measurements can be made through any material not conducting electricity including coatings, insulation materials, weather sheeting and even corrosion
products. It is a very useful characteristic that also enables high temperature non-destructive testing (NDT) inspections.

Inspection approach

The PEC instrument probe is placed against the metal weather sheeting (non-ferrous) of the insulated pipe or vessel. The geometry of the test object should be simple. A magnetic field is created by placing an electrical current in the transmitting coil of the probe. This field penetrates through the weather sheeting and magnetizes the pipe wall. The electrical current in the transmission coil is then
switched off, causing a sudden drop in the magnetic field.As a result of electromagnetic induction, eddy-currents will be generated in the pipe wall. The eddy-currents diffuse inwards and decrease in strength. The rate of decrease of the eddy currents is monitored by the PEC probe and is used to
determine the wall thickness.

Comparison with ultrasound wall thickness measurement

Both pulsed eddy-current and ultrasound wall thickness measurement have strong and weak points. The relevance of these strengths and weaknesses varies greatly from application to application.


Benefits at a glance

  • ƒNo loss of production, as inspection can take place while the inspection object is in service.
  • ƒReduced inspection costs, as insulation material does not need to be removed.
  • Significantly lowered costs for underwater inspections.
  • Speedy inspection, as surfaces do not require any preparation.
  • Good reproducibility of PEC readings at the same locations.
  • Plus minus 10% accuracy for corrosion detection under insulation and only plus minus 0.2% accuracy for corrosion monitoring.
  • Inspections within a temperature range from -100°C to 550°C (-150°F to 1000°F).
  • Inspection of objects with a wall thickness of 3 to 35 millimeter.
  • Inspection of objects with a pipe diameter above 75 millimeter.
Areas for application

Pulsed eddy-current can be effectively applied for corrosion 
monitoring and detection on pipes and vessels made of 
carbon steel or low-alloy steel without making contact with 
the steel surface itself.
ƒInsulated and/or coated equipments
  • ƒ Objects under high temperature conditions
  • ƒ Heavy corroded equipments
  • ƒ Offshore risers and caissons
  • ƒ Objects behind concrete fireproofing
  • ƒ Laminations
  • ƒ Annular rings
  • ƒ Bridges

Source: http://www.tuv.com/media/corporate/industrial_service/NDT_Pulsed_Eddy_Current_TUV_Rheinland.pdf

Wednesday, August 27, 2014

Refinery And Petrochemicals Integrated Development (RAPID) Project

Project Description

RAPID aims at building a world-scale integrated refinery and petrochemical complex.The proposed refinery will have a capacity of 300,000 barrels per standard day and will supply naphtha and liquid
petroleum gas feedstock for the RAPID petrochemical complex, as well as produce gasoline and diesel that meet European specifications.
The petrochemical units, on the other hand, will enhance the value of the olefinic streams coming from the RAPID steam cracker by producing various merchant grades petrochemicals products such as polyethylene, polypropylene, synthetic rubbers and other petrochemicals products.

Engineering and Construction

FEED Contract

Technip has been awarded a front-end engineering design (FEED) contract by PETRONAS for its proposed Refinery and Petrochemical Integrated Development (RAPID) project located in the state of Johor, Malaysia.

Technology Contract

CB&I was awarded a contract by PETRONAS for the license and engineering design work for five petrochemicals units. Lummus Technology will be providing technology for a world scale steam cracker complex comprising ethylene, butadiene, benzene, isobutylene and MTBE units.


Source: http://www.epcengineer.com/projects/details/2342/refinery-and-petrochemicals-integrated-development-rapid-project

Friday, August 22, 2014

Insulation is everywhere

Corrosion is undoubtedly one of the costliest problems facing industry today. Due to corrosion of piping and equipment under insulation many companies have to repair and/or replace major parts at a considerable cost, reported to run into billions of dollars annually. Clearly this considerably reduces the potential service life of industrial facilities. More frequently, essential shutdowns and overhauls impair plant efficiency, driving up operating costs.

Industrial plant insulation is everywhere. A medium-sized oil refinery contains 356 miles of insulated piping and more than 25 football fields worth 1.4 million ft² of insulated equipment, vessels and tanks. The plant temperature can easily exceed 1100°F, making insulation essential to protect people and maintain operational efficiency.

Prompt and proper maintenance
In many cases, insulation is not promptly or properly maintained,simply because it is not considered to be a risk. For years,industry has estimated that 10% to 30% of exposed insulation becomes damaged or missing within one to three years of installation. That percentage is likely to rise over time, depending on the operating environment and exposure to the elements. Many plant operators know that steam-generating capacity must be increased when it rains to continue to provide the heat the plant needs to operate efficiently.

Damaged insulation leads to increased heat losses and corrosion costs
The impact of damage can be substantial. In many cases, the actual reduction in heat loss is up to 40% more than expected. Damaged insulation cladding often allows water to penetrate into the insulation, which can cause corrosion. Costs due to corrosion,downtime and additional unanticipated energy losses are substantial. The costs of inspection and repair, which can often be carried out during operation, are negligible compared to the potential savings


Source:http://www.roxul.com/files/RX-NA_EN/pdf/Brochures%20and%20Sell%20Sheets/Industrial/Corrosion%20Under%20Insulation_web%20version.pdf

Saturday, August 16, 2014

Corrosion under Insulation/Fireproofing (CUI) - Corrosion Inspection


Source:http://www.ge-mcs.com/en/ndt-corrosion-inspection/ndt-corrosion-inspection-corrosion-under-insulationfireproofing-cui.html

Sunday, August 10, 2014

CUI vs. Energy Savings

Many industrial facilities—particularly oil refineries and petrochemical plants located near the ocean or a sea, or in areas where it rains a lot—suffer from both CUI and energy waste when insulation becomes damaged. When insulation systems age or become damaged, the caulk sealant cracks and the metal jacketing can open up gaps where rainwater—which may contain salt—intrudes.

If the insulation is an absorbent type and the service temperature is relatively low (below 300°F), then CUI can result. The heat loss from wet insulation may be as much as 10 times that for dry insulation. This can be a constant battle at older facilities because the caulk used to seal metal jacketing embrittles with time, and the metal jacketing itself may get dented, opening gaps and admitting water.

To prioritize maintenance work at refineries, petrochemical plants, and chemical plants, owners typically perform a risk assessment of the piping and equipment. These assessments help prioritize the most important items from the perspective of plant operation and/or plant safety. This risk assessment can be used to identify those areas where insulation needs to be repaired or replaced sooner rather than later since problems, such as CUI, can result in a partial facility shutdown or, worse, in a pipe or equipment leak.

To mitigate CUI, many refinery owners apply immersion-grade coatings to all piping and equipment that operate continuously at temperatures below 300°F. Some owners also require the use of non-absorbing insulation materials for all service temperatures. While the practice of using non-absorbing insulation is not prevalent everywhere, it is becoming increasingly common at facilities.

With today’s high energy costs, which make up approximately half the operations and maintenance costs at a typical refinery, maintaining insulation is a matter of economics. However, damaged insulation does not usually stop a facility from running. Operators simply increase the heat input to maintain process temperatures as required. Many refineries have had to increase the heat input during and immediately after heavy rains to compensate for water absorbed into the insulation at their facilities. One oil company engineer notes that it can take at least 3 days to dry out absorbent insulation following heavy rains at the company’s refineries. So even for pipes and equipment operating at temperatures above 300°F, where CUI is less likely to occur, energy waste from wet insulation is always a concern with water-absorbing insulation.

Using non-absorbing insulation materials is one approach to preventing wet insulation and CUI. Another approach is to add a chemical inhibitor to the absorbent insulation during manufacturing. Such chemical inhibitors reduce the probability of corrosion by inhibiting the corrosive effects of chlorides from saltwater and other sources. Insulation with chemical corrosion inhibitors is available in the marketplace.

A new technology that helps avoid CUI when using absorbing insulation materials is self-adhering laminate jacketing—thick tape that comes in 36-inch widths to match the pipe insulation width. The jacketing can be effectively sealed to itself with overlaps along the lap joints and with a minimum of 4-inch-wide, self-adhering tape—of the same material as the jacketing—applied at butt joints, junctions, and penetrations. Self-adhering laminate jacketing requires minimal caulk sealants and is available in weather-resistant, chemical-resistant forms. 

Since it uses only a thin-coated aluminum foil as opposed to aluminum sheet, laminate jacketing also uses much less aluminum, which has skyrocketed in price over the past few years. The laminate jacketing is flexible and dent-resistant. Since the adhesion of the material to itself is so tight, this new technology promises to be an effective way of keeping water from intruding into absorbent insulation materials on above-ambient applications.

Source:http://www.insulation.org/articles/article.cfm?id=IO070701

Happy Deepavali

The festival of light is here! May you be the happiest and may love be always with you. Happy Deepavali!